Context
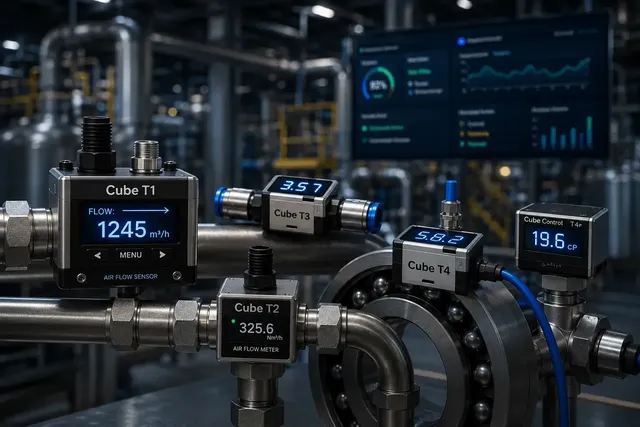
Unexpected equipment failures remain one of the biggest cost drivers in industrial manufacturing. Traditional monitoring systems typically react only after a fault has already occurred, leading to unplanned downtime, costly repairs, and inefficient maintenance processes.
Challenge
Manufacturers need greater visibility into the health of their equipment—not just to detect problems, but to anticipate them before they disrupt production.
The challenge was to create a smarter approach to industrial monitoring that combines real-time sensing, intelligent data analysis, and connected maintenance workflow.